A food-grade silicone oil should not be sprayed directly onto food-contact molds simply because it carries an NSF H1 incidental-food-contact registration. H1 status generally addresses unintended, trace contact from lubricated equipment parts; it does not by itself establish that a product is suitable for deliberate, repeated application to a mold surface where it will transfer to food.
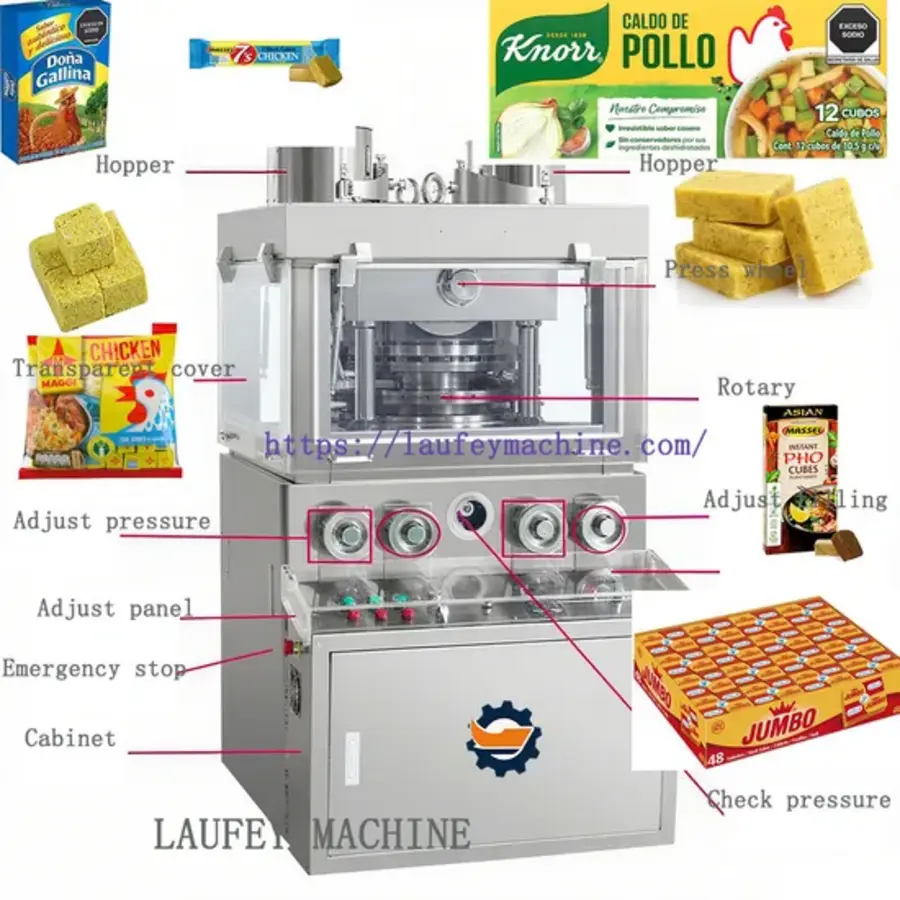
For a press with sticking and hardened residue, treat a sprayed lubricant as a process change requiring review, not as a quick maintenance fix. First identify why the product is adhering. Then, if a release substance is still needed, select and validate a product specifically authorized and documented for the intended direct food-contact release use, product type, process conditions, market, and application method.
Start with the sticking mechanism
Mold sticking is rarely caused by one factor alone. In compressed products such as bouillon cubes, adhesion can result from the interaction of formulation, moisture behavior, compaction, mold finish, pressing conditions, and cleaning effectiveness. Adding oil can temporarily change release behavior while concealing the original cause—or creating a residue cycle that makes the problem worse.
Separate the symptom into observable questions:
- Does material stick immediately after pressing, or does it build up gradually over a run?
- Is sticking uniform across all cavities, or concentrated in certain mold rows, punches, edges, or corners?
- Did the problem follow a formulation, ingredient, supplier, shift, or equipment change?
- Is the residue soft, oily, dry, glassy, compacted, or heat-hardened?
- Does material accumulate before the press, during filling, or mainly during ejection?
- Does the problem improve after cleaning and then return at a predictable point in the run?
A consistent pattern matters. Product that sticks in one area may point to worn tooling, uneven fill, alignment, surface damage, or a local process condition. Product that progressively coats all cavities may be more closely associated with formulation behavior, fines, moisture migration, inadequate cleaning, or an unsuitable release material.
Inspect the mold and process before changing chemicals
A structured inspection is more useful than trying several oils or sprays during production. Record findings by cavity, tooling set, date, product lot, and shift so the team can distinguish a recurring mechanical issue from a broader process issue.
Check tooling surfaces and ejection
Inspect food-contact mold surfaces, punches, and ejectors for scratches, pitting, corrosion, worn coatings, burrs, dents, and areas with a visibly different finish. Small defects can retain product and become nuclei for further buildup. Also review whether parts are properly seated and whether mold alignment, ejection, or scraping is consistent across the machine.
A scraper may remove loose material without resolving deposits that have compacted or hardened in corners and surface imperfections. If residue repeatedly survives normal scraping, determine whether the cleaning method is actually removing the film rather than merely dislodging the top layer.
Source: trimleaf
Check product condition and feed behavior
Review the approved product specifications and actual production records. Relevant factors can include particle-size distribution, fat content, moisture condition, ingredient temperature, agglomeration, fines generation, premix consistency, and hold time before pressing. The exact factors will depend on the formula and process, so they should be assessed against the site’s established specifications rather than assumed from a general rule.
Watch the material entering the molds. Poor distribution, bridging, overfill, uneven density, or accumulation on filling components can place excess material on mold edges. That material may be pressed into locations where it is difficult to eject and clean.
Review press settings and operating changes
Compare current operation with a period when release was acceptable. Review approved settings, tooling configuration, startup sequence, run duration, and changeover practices. If sticking began after a maintenance event, examine what changed: tooling, assembly, replacement parts, cleaning chemicals, calibration, or lubrication practices.
Do not bypass guards, interlocks, or established lockout procedures to inspect or adjust a press. Investigation of press motion, tooling alignment, and mechanical condition should be performed by qualified personnel under the site’s safety procedures.
H1 incidental contact is not the same as intentional mold release
The phrase “food grade” is broad and can be misleading. A lubricant can be appropriate for a food plant and still be inappropriate for spraying onto a product-contact mold.
NSF H1 registration is commonly used for lubricants in food-processing environments where incidental food contact may occur. Typical examples include lubricated seals, bearings, chains, valves, and other components where accidental transfer cannot be completely prevented. The intended use is incidental exposure, not necessarily a repeated application designed to transfer a coating to every product.
A release agent is a different functional use. It is intentionally applied to a surface to prevent food from adhering, and some portion may transfer to the product. Products marketed for direct food-contact release applications may be associated with NSF 3H registration or another applicable regulatory basis, but the designation alone should not end the review.
The plant must confirm the specific product’s approved use, not rely on a generic statement about silicone oil, an ingredient name, or a supplier’s marketing description.
| Question | Incidental-contact lubricant | Direct-contact release agent |
|---|---|---|
| Primary purpose | Lubricates equipment components | Promotes product release from a food-contact surface |
| Expected food transfer | Unintended and limited | Intentional, repeated transfer may occur |
| Typical decision basis | Equipment lubrication program | Product-contact, formulation, labeling, and process review |
| Is H1 alone sufficient for sprayed molds? | No—verify intended use with the supplier and internal food-safety team | Not applicable; verify the complete release-agent authorization and conditions of use |
Some silicone-based products may be promoted for release-related uses, and silicone fluids can appear in food-processing formulations. That does not mean every H1 silicone spray, bulk silicone oil, or maintenance lubricant is acceptable for direct application to a mold. Aerosol carriers, solvents, additives, propellants, application limits, and instructions can materially affect suitability.
What to verify before approving any release substance
A proposed mold-release material should move through formal change control. Include food safety, quality, regulatory, sanitation, engineering, procurement, and, where relevant, customer or brand teams.
Request the following from the supplier:
- Current technical data sheet and safety data sheet.
- The exact NSF registration category, if applicable, and the registered product identity.
- Written confirmation of the intended direct food-contact release application.
- The applicable regulatory basis for the countries where the finished food is sold.
- Stated conditions of use, including product type, food-contact surface, application method, and any limitations.
- Ingredient, allergen, processing-aid, labeling, and declaration information needed for the finished-product review.
- Cleaning compatibility information for the mold material, seals, coatings, and downstream equipment.
The internal review should also ask whether the release agent becomes an ingredient or processing aid under the applicable rules, whether it changes nutrition or label declarations, and whether customer specifications prohibit or limit it. These questions are jurisdiction- and product-specific. They require confirmation from the responsible regulatory and quality functions, not an assumption based on “food-grade” wording.
Validate the application, not just the product
Even an appropriate direct-contact release agent can fail if it is overapplied, inconsistently applied, or incompatible with the product. Validation should use a defined trial protocol before routine production use.
Set acceptance criteria in advance. They may cover release performance, visible residue, mold buildup over the planned run, product appearance, weight and dimension consistency, packaging behavior, sensory review where applicable, cleaning effectiveness, and absence of unacceptable effects on finished-product requirements.
Control the application method. A hand-held aerosol spray can produce variable coverage and overspray onto non-target equipment, guards, conveyors, or packaging areas. If a release agent is approved, the process should specify where it is applied, how application is controlled, how excess is prevented, and how the equipment is cleaned afterward.
Compare a documented baseline with the proposed change. If the test reduces sticking but increases mold deposits, affects product handling, or complicates sanitation, it has not solved the full problem. Similarly, if vegetable oil accelerated buildup in prior trials, do not assume silicone will behave differently without a controlled evaluation; the carrier, film properties, dosage, and product interaction may all differ.
Cleaning and sanitation must be part of the decision
A release coating changes the soil profile on molds. It may hold fines, alter how residues adhere, or require changes to the cleaning sequence. Before approval, sanitation personnel should assess whether the proposed substance can be effectively removed using the site’s validated cleaning approach and whether it affects inspection of mold surfaces.
Do not alter cleaning chemicals, concentrations, contact times, or sanitation steps based only on lubricant supplier advice. Cleaning changes should follow the facility’s chemical-compatibility, sanitation-validation, and food-safety procedures. Verify that mold materials, coatings, seals, and nearby components remain compatible with both the release agent and the cleaning system.
A practical decision path
- Contain the immediate issue. Use approved cleaning and production controls; do not introduce an unreviewed spray onto food-contact molds.
- Characterize the failure. Map where, when, and how residue develops.
- Inspect equipment condition. Check mold finish, tooling wear, alignment, filling, and ejection.
- Review product and process changes. Compare formulation, material condition, settings, and operating records with known-good runs.
- Correct the identified cause where possible. Repair or restore tooling, adjust approved process conditions, or address feed and cleaning issues through controlled procedures.
- Evaluate release agents only if needed. Obtain written use authorization and complete food-safety, regulatory, quality, and sanitation review.
- Run a controlled validation. Define application controls and acceptance criteria before the trial.
- Document and monitor. Add the approved material to chemical control, preventive maintenance, sanitation, training, and verification records as applicable.
When to stop and escalate
Stop the proposed direct-spray approach and involve qualified food-safety and regulatory personnel if the product documentation is unclear, the supplier cannot confirm direct food-contact release use, the material could affect labeling or customer requirements, or trial results show persistent residue, cleaning problems, or product changes.
The useful distinction is simple: an H1 lubricant may be appropriate where incidental contact is possible, but direct coating of food-contact molds is an intentional food-contact application. Solve the sticking mechanism first, then approve and validate any release system as a controlled part of the food process.
References
- Food-grade silicone oil in food processing : r/foodscience. (n.d.). https://www.reddit.com/r/foodscience/comments/1oxgwbr/foodgrade_silicone_oil_in_food_processing
- Silicone oil in food processing : r/FoodSafetyPros. (n.d.). https://www.reddit.com/r/FoodSafetyPros/comments/1oxgort/silicone_oil_in_food_processing
- Understanding Food Grade Silicone Lubricants. (n.d.). https://jax.com/understanding-food-grade-silicone-lubricants
- Food grade lubricants. (n.d.). https://wiki.anton-paar.com/en/food-grade-lubricants
- Food Grade Lubrication. (n.d.). https://tractian.com/en/glossary/food-grade-lubrication
- Pure Silicone FLuid NSF H1 Food Grade. (n.d.). https://www.clearcoproducts.com/product/psf%E2%80%90350cst-pure-silicone-fluid-nsf-h1-food-grade-2
- Food Grade Silicone Spray Lubricant NSF H1 | Jet-Lube. (n.d.). https://www.jetlube.com/product/food-grade-silicone-food-grade-lubricant-nsf-h1
- Food Grade Silicone Lubricant sfg-350. (n.d.). https://www.clearcoproducts.com/product/sfg-350-food-grade-silicone-lubricant-nsf-h1